
Barrier Bags
KNF FLEXPAK Corporation and KNF Clean Room Products Corporation manufacture custom barrier bags for applications that require protection from moisture, gases, chemicals, contaminants, and other environmental conditions. With more than 50 years of flexible packaging experience, KNF produces Nylon, polyethylene, and multilayer film products for industrial, food, medical, pharmaceutical, aerospace, electronics, and cleanroom applications.
Custom Barrier Bags for Specialized Packaging Requirements
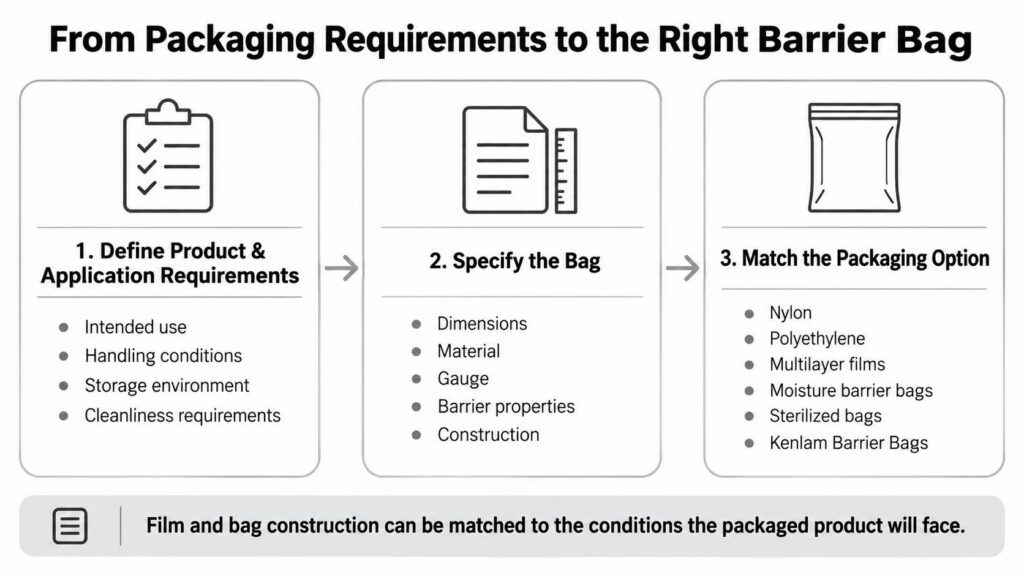
Packaging requirements can vary significantly based on the product, handling conditions, and storage environment. KNF provides custom barrier bags made to meet specific packaging needs, with options for material, size, gauge, construction, and other specifications.
KNF's film extrusion and converting capabilities allow customers to select materials suited to their applications. Whether you need packaging for industrial components, chemicals, food products, or sensitive equipment, KNF can help identify an appropriate film and bag construction.
Custom barrier bags can also be produced in different sizes and thicknesses, giving you greater control over how products are packaged, stored, and transported.
Barrier Protection Against Moisture and Environmental Exposure
Moisture, gases, chemicals, and other environmental factors can affect products during storage and transportation. KNF offers film materials with barrier properties suited to specific packaging requirements.
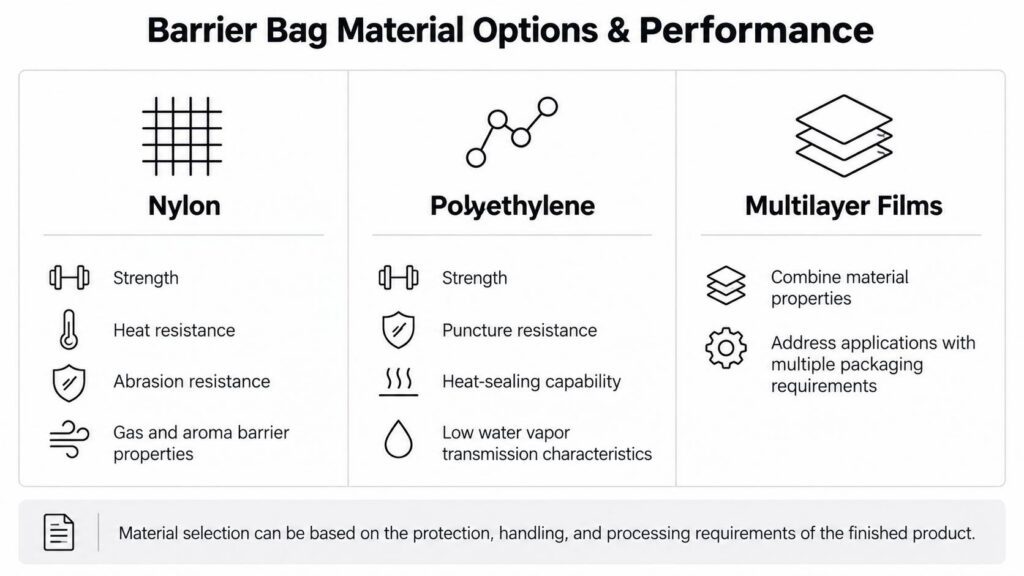
Polyethylene films provide low water vapor transmission characteristics, making them useful for applications that require moisture control. Nylon films offer gas and aroma barrier properties along with resistance to chemicals, abrasion, and demanding handling conditions.
For products that require added moisture protection, moisture barrier bags can provide a practical packaging option. KNF can help match the film construction to the conditions your packaged products will face.
Materials and Barrier Bag Options
KNF works with Nylon, polyethylene, and multilayer films to produce flexible packaging products for a range of industries. Each material provides different performance characteristics, allowing you to select the option that fits the application.
- Nylon: Provides strength, heat resistance, abrasion resistance, and gas and aroma barrier properties.
- Polyethylene: Offers strength, puncture resistance, heat-sealing capability, and low water vapor transmission characteristics.
- Multilayer films: Combine material properties to address applications with multiple packaging requirements.
KNF also offers products such as Kenlam Barrier Bags and related Kenlam packaging options. Material selection can be based on the protection, handling, and processing requirements of the finished product.
Barrier Bags for Medical, Pharmaceutical, and Cleanroom Applications
Sensitive products require packaging that supports cleanliness and controlled handling. KNF Clean Room Products provides packaging products for medical, pharmaceutical, laboratory, electronics, and other controlled environments.
For applications involving sterilization, KNF offers sterilized bags and sterilization packaging products, including HDPE and HDPE/Tyvek options. These products serve applications where packaging cleanliness and sterilization requirements are important.
KNF also manufactures UltraClean products in ISO Class 5 clean rooms for applicable cleanroom packaging needs.
Applications for Barrier Bags
KNF barrier packaging supports a variety of applications, including:
- Medical and pharmaceutical packaging
- Chemical packaging
- Aerospace and composite manufacturing
- Electronics
- Food processing
- Industrial packaging
- Cleanroom applications
Why Choose KNF for Barrier Bags?
KNF brings extensive film extrusion, converting, and flexible packaging experience to each project. The company offers custom manufacturing capabilities along with Nylon, polyethylene, and multilayer film options. Its Quality Management System is ISO 9001:2015 certified, while applicable UltraClean products are manufactured in ISO Class 5 clean rooms.
This combination of material knowledge, converting capabilities, and specialty packaging experience gives you a direct source for barrier bag requirements.
Request Custom Barrier Bags from KNF Extruding Nylon Film
The right barrier bag starts with the requirements of your product and application. Share your desired dimensions, material, gauge, barrier properties, cleanliness requirements, and intended use with KNF FLEXPAK or KNF Clean Room Products. The team can help identify the appropriate packaging option for your needs.
Contact KNF today to discuss custom barrier bags for your application.